

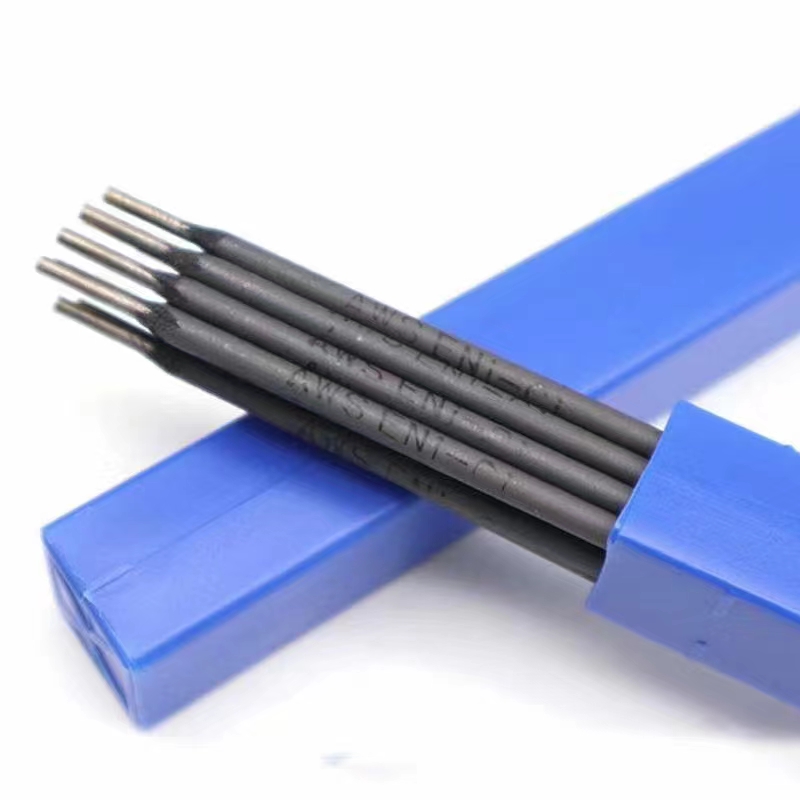
Copper Bridge ENi-C1 Cast Iron Stick Electrode
DESCRIPTION
Copper Bridge ENi-C1 is a nickel-core electrode for welding normal grades of cast iron. The weld metal is soft and easily machinable, and it can be used on cold or slightly preheated material for joining cast iron, correcting castings, and repairing broken parts.
▶ AVAILABLE DIAMETERS
3/32 in, 1/8 in, 5/32 in, 3/16 in
2.5 mm, 3.2 mm, 4.0 mm, 5.0 mm
▶ PACKAGING
2.2 lb, 4.4 lb, 11 lb
▶ APPLICATIONS
Mainly used for welding thin cast-iron parts
and repairing broken parts.
▶ WELDING PROCESS
SMAW / Stick Welding
▶ POLARITY
AC or DC+
▶ WELDING POSITIONS
Flat, horizontal, vertical, overhead
CHEMICAL COMPOSITION OF DEPOSITED METAL (WT.%)
| Element | C | Mn | Si | Ni | Fe |
| AWS Requirement | ≤2.0 | ≤2.5 | ≤4.0 | ≥85 | ≤8.0 |
| Copper Bridge Typical | 0.65 | 0.05 | 1.56 | 95.8 | 2.16 |
MECHANICAL PROPERTIES OF DEPOSITED METAL
| Property | AWS Requirement | Copper Bridge Typical |
| Weld Deposit Hardness | 150-200 HB (machinable) | 180 HB |
| Tensile Strength | Not specified | 345 MPa (50 ksi) |
| Elongation | Not specified | 8% |
RECOMMENDED WELDING PARAMETERS
| Diameter | 3/32in(2.4 mm) | 1/8 in(3.2mm) | 5/32in(4.0mm) | 3/16in(5.0mm) |
| Flat /HorizontaI (A) | 50–70 | 70–100 | 100–130 | 130–170 |
| Vertical/Overhead (A) | 40–60 | 60–90 | 90–120 | 120–150 |
NOTES
1. Bake electrodes at 120°C (248°F) for 1 hour before welding.
2. Peen each bead to relieve stress and help avoid cracking.
 Home
 Tel
 Product